
Hardness on a pressure vessel weld, a length of track or a mill housing has to be verified where the part already sits. Nobody is cutting a coupon out of a finished fabrication to satisfy a bench tester, and by the time a sample reaches a laboratory the question that prompted the test has usually stopped being urgent.
Portable Brinell testing exists for that gap. The Telebrineller is one instrument built around it, and the way it produces a number is worth understanding before deciding whether a field reading will hold up in a report. What follows is the method, the conditions that govern its accuracy, the places it should not be used, and how it sits beside the other two families of portable hardness testing.
Why a Hammer Blow Can Give a Defensible Brinell Number
The obvious objection to hand-held indentation testing is force. Brinell hardness is defined by a known load pressed into a surface, and no one swinging a hammer is applying a known load. Hit harder and the impression grows.
The Telebrineller sidesteps that instead of trying to solve it. The instrument holds a calibrated test bar directly above the workpiece with a single steel ball between them. One blow on the anvil drives that ball into the bar and the specimen at the same moment, so both surfaces receive exactly the same impact. Whatever the force of the blow was, it went into both impressions equally, which means it cancels when the two are compared. The hardness is read from the ratio of the impression diameters, not from the strength of the strike.
The arrangement is not improvised, either. ASTM A833 covers indentation hardness of metallic materials by comparison hardness testers, and it applies specifically to portable comparison testers that use test bars standardized to ASTM E10 as the basis for comparison. The same standard states that the impression force in this kind of test is normally an impact load applied by striking a hammer, which is precisely the arrangement described above. Worth knowing as well: ASTM E110, the standard usually cited for portable Rockwell and Brinell testers, explicitly does not apply to instruments that work this way, and points to A833 instead.
A spacing mechanism, released by a spring catch and button, then moves the bar along to clean metal so the next test does not land on a used area. The whole system travels in a case under ten pounds and needs no power at all, which is the practical reason it ends up on scaffolding and in trenches rather than on a bench.
What Actually Decides the Number
Because the method is comparative, the reference bar is half of every measurement. Its quality sets the ceiling on the result, and the choice made in the first ten seconds of the test matters more than anything the operator does afterwards.
Standard test bars hold a uniform hardness within two percent of the BHN etched on the end. They are ground from assorted carbon steel alloys to a 9/16 inch square, and low value bars are also available in aluminum. Impression diameters are converted through the King-Scan computerized calibration system, whose accuracy complies with the National Institute of Standards, and the value is rounded to the nearest standard BHN at 0.05 mm intervals against the Brinell hardness number table of ASTM E10 before being etched on the bar.
The same logic explains the material rule. A bar should be of the same general material as the specimen, and where non-ferrous metals are tested against carbon steel bars the designated correction factors for impact error have to be applied rather than ignored. Skipping that step is the most common way a field reading turns into a number nobody can defend later.
That pair of rules is what decides the bar set a crew carries. A shop that only ever checks one grade of carbon steel in a narrow hardness band needs very few bars. A crew that walks between mild steel fabrications, quenched and tempered plate and the occasional non-ferrous fitting needs the range covered in steps close enough that every job lands inside somebody’s fifteen percent window, plus the correction factors written down rather than remembered.
How Many Bars a Crew Actually Needs
The fifteen percent window turns an abstract rule into a shopping list. Standard bars are available in values running from a little over 100 BHN up past 600, in steps close enough that most practical hardness ranges can be bracketed, and the set you carry is simply the answer to one question: which parts of that span does your work actually land in.
A fabrication shop working a single grade of structural steel usually sits inside a narrow band and can cover it with a handful of bars. A service crew that moves between mild steel, quenched and tempered plate, hardfaced surfaces and the occasional non-ferrous fitting needs the span covered more densely, because every job has to find a bar within fifteen percent of whatever it meets that day. The bars that never get used are cheaper than the trip back to the shop for the one that was missing.
Two practical points follow. Bars are consumable in the sense that each one accumulates impressions and eventually runs out of clean surface, so a working set includes replacements for the values used most. And where non-ferrous work is routine rather than occasional, the correction factors for impact error belong written on the inside of the case lid, not in somebody’s memory.
What Travels in the Case
The instrument is deliberately simple, and every part in it is replaceable. Knowing what each piece does makes it obvious why the system survives conditions that would end a powered tester.
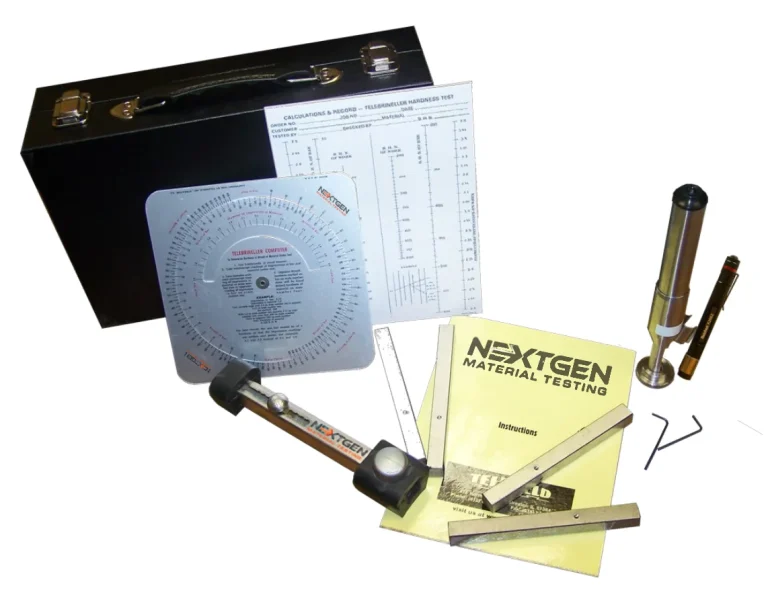
At the working end there is the bar holder assembly, the anvil that takes the hammer blow, and the impression ball that sits between the test bar and the workpiece. Rubber front and rear pieces cushion the instrument against the specimen. The spacer button, block and spring form the mechanism that advances the bar to fresh metal between tests, and a bar tube carries the spares. Measurement is handled by the microscope and the calculation and record pad, an LED flashlight covers the fact that field work rarely happens in good light, and a calibration disk keeps the optics honest. The computer converts the two measured diameters into a BHN.
The absence of anything electronic in the load path is the point. There is no battery to fail in the cold, no transducer to drift, and no calibration state that can quietly go stale between services. The only thing that has to hold its value is the bar, and the bar carries its value etched on the end where anyone can read it.
Reading the Impressions Without Adding Error
Everything up to this point produces two small craters in metal. The number comes out of measuring them, and that is where an otherwise correct test quietly loses its accuracy.
Brinell impressions are rarely perfectly round, which is why the standard practice is to measure two diameters at right angles to each other and use their mean rather than trusting a single reading. On the Telebrineller both impressions get the same treatment, the bar and the workpiece alike, since a careful measurement on one side and a casual one on the other breaks the comparison just as effectively as picking the wrong bar.
None of this is unique to comparison testing. It is ordinary Brinell discipline carried out of the laboratory, where the bench, the lighting and the fixed optics used to do half the work for the operator.
Welds, Fillets and the Heat Affected Zone
Fillet welds and other confined joints are exactly the geometry that portable testing exists for, and exactly the geometry a standard instrument head cannot sit on. The Halteman Filletester is made for that case and is used together with the Telebrineller. Test bars are cut in half for easier handling in the joint, and the impressions are measured with the 5/8 inch diameter end of the microscope nose piece.
For harder specimens the impression ball is available in tungsten carbide as well as the standard version, which keeps the indenter itself from becoming the thing that deforms.
Where the Method Reaches Its Limit
One limit deserves stating plainly, because it decides whether this is the right instrument for a given weld at all. The heat affected zone alongside a weld is narrow, a fraction of a millimeter in many joints, and a Brinell impression is large by comparison. Where the specification is asking about the joint as a whole, that is fine. Where the heat affected zone itself is the thing being qualified, an impression that spans both the affected metal and the parent material returns an average and can read lower than the peak hardness actually present. That case calls for a small indent method instead, and the section below sets out which one.
Choosing Between the Portable Methods
Comparative Brinell is not the only way to read hardness away from a bench, and the three portable families answer to different physics. The cleanest way to choose between them is to ask what each one actually measures, because that is what decides where each stops being trustworthy.
The Telebrineller measures a Brinell impression directly. A real ball indentation is made and its diameter is compared with one of known value, so what comes out is a Brinell number arrived at the Brinell way, which matters when a specification calls for BHN rather than a figure converted from something else. The cost is a visible impression and the need to carry a bar close to the hardness you expect.
An ultrasonic contact impedance tester measures something else entirely. A Vickers diamond on a vibrating rod is pressed into the surface, and the shift in the rod’s resonant frequency gives the hardness. That shift depends on the contact area of the indentation and on the elastic modulus of the material, which is the reason a UCI instrument has to be matched to what it is reading. The indentation it leaves is small enough that it has to be found under a microscope, so this is the method for foil, thin coatings, hardened and nitrided layers, and finished parts that must not carry a mark. It is also the one to reach for when the narrow heat affected zone beside a weld is what has to be read, rather than the joint as a whole.
A Leeb rebound tester measures a velocity ratio. An impact body is fired at the surface and the instrument compares rebound velocity with impact velocity, and the resulting HL value converts into Rockwell, Vickers, Knoop, Brinell or Shore. It is the fastest of the three on large fixed structures, and on the LeebGen 3000 the impact direction sensor holds the result within four HL whichever way the probe is pointed, which is what makes an overhead or sideways reading agree with one taken from above. The method is covered by ASTM A956, which addresses Leeb hardness testing of steel, cast steel and cast iron rather than metals in general.
Two things separate the three in practice more reliably than any specification sheet. The first is what the part weighs and how thick it is. Both the rebound and the ultrasonic methods put energy into the specimen and read what comes back, so a thin or lightly supported section moves under the probe and biases the result downward, which is why both carry minimum mass and thickness conditions and procedures for coupling a light part to a solid support. A comparison Brinell test is indifferent to that in a different way: it needs enough material to take a clean impression without the back face distorting, and it needs the instrument held square.
The second is what the number on the display actually is. A Leeb instrument reports HL and a UCI instrument reports a comparative value, and both then convert into the scale you asked for using empirical tables. Conversion between hardness scales is an approximate process, and standards that publish those tables say so plainly. If a drawing calls out Brinell and an inspector reads Brinell, nobody has to defend a conversion step. If the same figure arrives converted from a rebound reading, that step is part of the record whether it is written down or not.
Keeping Field Results and Bench Results in the Same File
A portable reading is only worth taking if it can sit in the same record as a laboratory result without an argument about where it came from. That is a documentation question as much as a technical one, and it is worth settling before the crew leaves rather than when the file is reviewed.
With a comparison tester the traceability lives in the bar. Each one carries its value etched on the end, set through a calibration system whose accuracy complies with the National Institute of Standards and rounded against the Brinell table of ASTM E10. That etched number, and the certificate behind it, is what a reviewer can actually follow. The blow itself is never measured and never needs to be, but it also means the instrument is not verified the way a bench machine is, so the honest description of a field result is a comparison against a traceable reference rather than a primary measurement.
In practice that shapes what goes into the record. Note the bar used and its etched BHN, the material and condition of the specimen, whether a correction factor was applied, and the two diameters actually measured rather than only the converted result. A file with those entries survives a question months later. A file with a bare hardness number does not.
It also sets the boundary for when the work belongs back on a bench. Acceptance testing against a tight specification, arbitration between two parties, and anything feeding a material certificate are jobs for a verified bench Brinell tester with direct and indirect verification behind it. The portable instrument is for confirming, screening and catching problems early, which it does in minutes and at the joint.
Where a Portable Brinell Test Earns Its Place
The Telebrineller was developed for welding crews out of fifty years of site experience, and that origin still describes the work it suits best. Hardness on a joint has to be confirmed in place, often outdoors, frequently on something that will never move again, and the answer is needed while the crew is still standing there. No power, no specialist training and a case under ten pounds are not conveniences in that setting, they are the conditions that decide whether the test happens at all.
Laboratories and quality control departments use it differently, as the portable half of a hardness program that otherwise runs on bench equipment. The certified bars are what let a field reading sit in the same file as a bench result, since every bar carries a traceable value etched on its end rather than a number somebody assumed. Construction, manufacturing and engineering teams use it for the same reason: the structure stays where it is and the instrument comes to it.
Machines Behind This Article
 Portable Hardness TestersTelebrineller – Portable Brinell Hardness Testing SystemNextGen Telebrineller is a portable Brinell hardness testing system for field use, welding crews, and QA teams that need fast BHN checks outside a stationary lab....View product
 Brinell Hardness TestersBrinGen 3000 Series – Digital and Automatic Brinell Hardness TesterBrinGen 3000 Series is a digital Brinell hardness tester for evaluating indentation resistance in metals such as cast iron, unquenched steel, non-ferrous metals,...View product
 Portable Hardness TestersNG-LeebGen 3000 – Portable Leeb Rebound Hardness TesterLeebGen 3000 is a portable Leeb rebound hardness tester for non-destructive metal hardness measurement in the lab, shop, or field. Designed to support ISO 18625,...View product
 Portable Hardness TestersUH200 – Ultrasonic Contact Impedance Hardness TesterUH200 is a portable ultrasonic contact impedance hardness tester for fast, accurate hardness checks on metals and finished components. Using a 136° Vickers diamond...View product
 Brinell Hardness TestersHardness Test Blocks, Indenters and AccessoriesHardness test blocks, indenters, and accessories support daily verification and reliable operation of metal hardness testing systems. The range includes certified...View product
 Brinell Hardness TestersBrinGen Scope – CCD Brinell Measuring ScopeBrinGen Scope is an advanced CCD Brinell measuring scope for manual or digital Brinell hardness testing systems. Designed to work with a computer or laptop, it...View product
 Brinell Hardness TestersMetallography ConsumablesMetallography consumables cover the materials needed for sectioning, mounting, grinding, polishing, etching, and cleaning specimens before microscopic examination....View product
 Portable Hardness TestersSurface Roughness TestersNextGen Surface Roughness Testers are portable profilometer-style instruments for measuring surface texture on machined parts and manufactured components. They help...View product